AirAccess Access Control as a Service Platform with Auto-Cell Networking (ACasS)
Enterprise Hosted Platform - MVPAccess™
New! Napco Access 1 & 2-Door Controllers
Please contact us directly or visit our FAQ page or Video Library.
Toll Free 800-645-9330
Phone 631-842-9400
Fax 631-842-9135
Email: sale@safehomeexpert.com
sale@safehomeexpert.com (Latin America)
Sign up for integrator training seminars. 2 days and 3 day online courses are available from our directory indexed by product.
Learn MoreOffer the one access control solution powerful and flexible enough to protect all of your clients. Continental Access provides state-of-the-art access control software and hardware in an easy-to-implement and easy-to-use access control solution that seamlessly integrate with a wide range of facility management products.
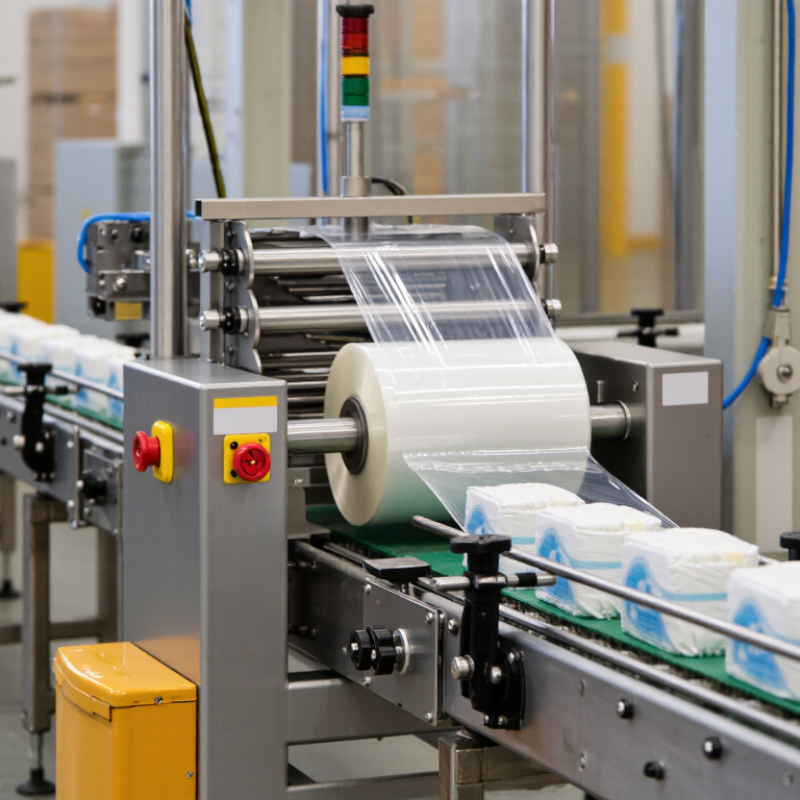
Learn MoreChoosing the right High-speed diaper packing machine is not simply a speed comparison. It is a production decision involving hygiene, accuracy, labor, materials, and long-term reliability. A machine may advertise 600 packs per minute, yet real output can fall when diaper sizes change or film tension varies. Numbers need context.
In practical factory evaluations, I would inspect the complete packaging process, not only the main frame. Watch how products enter the feeding system. Check whether packs remain aligned during compression. Examine sealing edges, date coding, film tracking, and finished-pack handling. Small defects become expensive when repeated across thousands of packs. The machine should also support stable operation, quick size adjustment, and accessible maintenance points. Operators should understand these functions without relying on guesswork.
Safety and compliance deserve equal attention. Confirm electrical standards, guarding, emergency stops, documentation, and sanitation requirements for the intended market. Ask for recorded test results, sample packs, spare-parts information, and references from comparable facilities. A supplier’s response to difficult questions often reveals more than its brochure. Do not trust speed alone. It can be misleading.
There is no perfect machine. A faster model may require more skilled maintenance or higher film quality. A lower-cost option may create hidden downtime. Buyers should compare total ownership costs, including energy, training, waste, service, and future expansion. I may overlook a detail without a site visit, so every recommendation should remain open to verification. The best choice balances proven performance, product protection, operator safety, and realistic factory needs.
A high-speed diaper packing machine typically handles 60–120 packs per minute. However, this figure is rarely constant in daily production. Actual speed depends on diaper size, pack count, film thickness, and folding accuracy. A machine running at 120 packs per minute may slow to 80 when producing larger bundles. Speed is conditional.
In factory trials, measure sustained output rather than the highest screen value. Watch the infeed conveyor, stacking unit, sealing jaws, and discharge section for at least one hour. Record stoppages, rejected packs, film breaks, and operator adjustments. Measure it live. A reliable machine should maintain stable seals and neat edges at the selected speed. Loose wrapping can damage transport efficiency and customer confidence.
A practical evaluation also includes changeover time. Switching from a small newborn pack to a larger economy pack should not require excessive manual alignment. Ask for test data using your own diaper dimensions and packaging materials. Check whether the quoted 60–120 packs per minute includes rejected products or only accepted packs. That detail matters. Some specifications look impressive but hide frequent micro-stops. I have seen fast equipment lose production through small sensor delays and awkward cleaning access. This is easy to overlook. Choose performance that workers can repeat safely, not merely a peak number recorded during a short demonstration.
Choosing a high-speed diaper packing machine starts with the line’s real output, not the machine’s headline speed. Vorne’s OEE benchmark guidance places world-class performance at 85%, while many plants operate near 60%. An OEE target above 80% is demanding but practical when speed, availability, and quality are measured together.
Calculate required capacity from saleable packs, not total packs. For example, a line producing 600 packs per minute at 82% OEE delivers about 492 effective packs per minute. Include planned stops, film changes, rejected packs, and short cleaning cycles. PMMI’s packaging automation reports repeatedly identify labor availability and unplanned downtime as major investment drivers. That makes quick changeovers and accessible maintenance important, not optional features.
Leave controlled headroom. A machine rated at 650 packs per minute may suit a 500-pack-per-minute line better than a 900-pack model. Excess capacity can increase energy use, unstable feeding, and unnecessary capital cost. Ask suppliers for verified speeds using your diaper dimensions, film structure, and pack count. Request a factory acceptance test with recorded OEE conditions.
Reality is messier. OEE can look strong while operators bypass minor stops or record defects inconsistently. Review downtime codes weekly, and separate speed loss from material problems. The target may need adjustment after three months of production data. That is not failure; it is better engineering.
Choosing a high-speed diaper packing machine starts with the pack format, not the advertised speed. A 20-diaper bag needs shorter film indexing, smaller sealing jaws, and faster changeovers. An 80-diaper bag requires deeper forming space, stronger film handling, and stable compression. According to Smithers’ “The Future of Flexible Packaging to 2028,” the global flexible packaging market was valued at about $201.8 billion in 2023. That scale reflects a clear need for reliable, material-efficient systems.
Film compatibility can decide whether the line performs well. Polyethylene films, breathable backsheet laminates, and printed multilayer films behave differently under heat and tension. Check seal temperature, coefficient of friction, film thickness, and web width before purchasing. A machine may run at 400 bags per minute on lightweight film, but speed can fall sharply with thicker laminates or unstable bag shapes. Real production trials matter more than brochures.
Packers should also compare servo control, automatic film centering, and tool-free size changes. PMMI industry reports repeatedly identify uptime, labor efficiency, and quick changeovers as major packaging investment priorities. Measure actual output after sealing, not only the infeed rate. That distinction is often missed. A 20–40 diaper format may favor high throughput, while 60–80 diapers may favor compression accuracy and seal strength. I would test at least three film structures and several diaper absorbency levels. One overlooked detail can become the most expensive problem.
How to Choose a High Speed Diaper Packing Machine?
Counting accuracy should be tested with real diapers, not only an empty machine. Run different sizes, thicknesses, and package quantities at working speed. Check sensor response, missed counts, double counts, and rejected packs. A practical trial should record results over several hours. Small errors multiply.
Sealing quality deserves equal attention. Inspect seal width, wrinkles, open corners, and film damage after continuous operation. Ask for temperature, pressure, and dwell-time controls with readable settings. Test finished packs through gentle compression and peel checks. A strong seal should remain closed during handling, storage, and transport. I would also examine changeover performance, because unstable settings often appear after switching diaper sizes. No machine performs perfectly every day.
CE marking can support regulatory compliance when the machine meets applicable safety and conformity requirements. Request the Declaration of Conformity, technical documentation, and safety instructions. Do not treat a CE mark as proof of counting accuracy or sealing performance. ISO 9001 certification indicates a quality management system, not automatic machine excellence. Check whether production records, inspections, calibration, corrective actions, and staff training are controlled. Ask for recent test records and service procedures. Clear evidence is more useful than polished claims. A factory visit may reveal details that documents miss. akunner
| Evaluation Dimension | Recommended Benchmark | How to Verify | Why It Matters |
|---|---|---|---|
| Production Speed | Select a rated output that is at least 15–20% above the required sustained output. For many medium-to-high-speed diaper bagging lines, a practical target is approximately 80–150 bags per minute, depending on pack count and product size. | Request a witnessed production test using the actual diaper dimensions, pack count, film, and operating speed. | Rated maximum speed may be higher than the stable production speed achieved during continuous operation. |
| Counting Accuracy | Target at least 99.5% pack-count accuracy under stable feeding conditions; high-volume applications should evaluate whether 99.8% or better is achievable. | Run a statistically meaningful trial, record under-counts and over-counts separately, and inspect the count sensor, encoder, and reject logic. | Incorrect counts create customer complaints, rework, material loss, and possible compliance issues. |
| Counting Technology | Use synchronized photoelectric sensors, servo-controlled feeding, and an electronic counting system with recipe-based settings. | Check sensor response, product-spacing control, count memory, alarm records, and automatic rejection of incomplete packs. | Accurate detection and synchronized motion reduce missed counts when products overlap or vary slightly in thickness. |
| Sealing Quality | The seal should be continuous, clean, and free from wrinkles, burn-through, open corners, and contamination. Seal strength must be validated for the selected polyethylene or co-extruded film. | Perform visual inspection, leak or burst testing where applicable, and seal-strength testing under normal and worst-case temperature and speed settings. | Weak or inconsistent seals can cause pack opening, product contamination, and transport damage. |
| Temperature Control | Use independent temperature control for sealing zones, with adjustable parameters and over-temperature protection. Temperature stability should be checked during continuous operation. | Compare the displayed temperature with an external calibrated measuring device and review temperature alarms during a production trial. | Stable heat reduces seal variation when film thickness, ambient temperature, or line speed changes. |
| Film Compatibility | The machine should support the intended film type, width, thickness range, roll diameter, and printing or registration requirements stated in the technical specification. | Test the exact packaging film and confirm web tension, tracking, roll loading, registration accuracy, and film-change procedure. | A machine optimized for one film structure may produce wrinkles or unstable seals with another structure. |
| CE Marking | For machinery supplied to the European Economic Area, require a valid CE conformity process, Declaration of Conformity, risk assessment, technical documentation, and operating instructions in the required languages. | Verify the machine nameplate, Declaration of Conformity, applicable EU legislation, safety circuits, guards, emergency stops, and technical file availability. | CE marking indicates that the manufacturer declares conformity with applicable EU requirements; it is not a substitute for checking machine safety. |
| Safety System | The machine should include interlocked guards, accessible emergency stops, safe access to heated areas, overload protection, and controlled restart after a safety trip. | Carry out a documented safety-function test and confirm that opening a guard stops hazardous motion as intended. | Safety controls protect operators during film loading, cleaning, adjustment, and fault recovery. |
| ISO 9001 Quality System | Prefer a supplier with a current ISO 9001 certificate issued by an accredited certification body and a documented quality-management scope covering machine design or manufacturing. | Check certificate validity, certification scope, issuing body, audit status, traceability procedures, nonconformity handling, and final inspection records. | ISO 9001 supports consistent processes, corrective action, document control, and traceable quality management. |
| Changeover Time | A well-designed line should provide tool-less or quick-adjust settings where practical. A typical target for a routine size or count change is approximately 15–30 minutes after operator training. | Time the changeover using the required format, count, film, and operator procedure; include cleaning and first-article approval. | Shorter changeovers improve equipment utilization and reduce material waste between production orders. |
| Automatic Rejection | The system should detect and reject under-counted, over-counted, unsealed, or incorrectly positioned packs without stopping the entire line whenever feasible. | Test each fault type independently and confirm that rejected products cannot be mixed with accepted products. | Reliable rejection protects finished-product quality while maintaining high throughput. |
| Control and Data Records | Use a PLC/HMI system with password-protected recipes, production counters, alarm history, downtime records, and data-export capability where required. | Review user permissions, recipe recovery, alarm timestamps, counter accuracy, and compatibility with the plant data system. | Recorded data supports troubleshooting, production analysis, quality investigations, and operator accountability. |
| Maintenance and Spare Parts | Require preventive-maintenance schedules, electrical and pneumatic diagrams, recommended spare-parts lists, troubleshooting guides, and remote or on-site technical support. | Ask for lead times for critical parts such as sensors, heaters, belts, cutting blades, sealing components, and drive elements. | Clear maintenance documentation reduces downtime and helps operators restore production safely. |
| Acceptance Criteria | Define measurable limits before purchase, including sustained speed, count accuracy, seal quality, reject rate, changeover time, noise, and safety-function performance. | Include the criteria in the FAT and SAT documents and approve the machine only after the agreed tests are passed. | Clear acceptance criteria prevent disputes and ensure that the purchased machine meets actual production needs. |
Note: The numerical values above are practical procurement benchmarks for evaluation. Actual performance depends on diaper dimensions, pack count, film structure, operator skill, machine configuration, and production conditions.
Speed alone misleads. A reliable machine should complete product changeovers in under 30 minutes, not just advertise high output. During factory trials, time the full process: stopping, cleaning, adjusting guides, changing film, and restarting. Ask operators to perform the changeover, because real results often differ from supplier demonstrations. Record the first saleable pack, not the first moving pack. That detail matters.
Energy use deserves equal attention. Measure electricity, compressed air, and heating demand during production and standby periods. A machine with efficient servo motors may reduce power consumption, but only if settings are optimized and maintenance is consistent. Check kilowatt-hours per thousand packs under normal loading. Request test data from comparable production conditions. Numbers without operating details are weak evidence.
Total cost of ownership includes more than the purchase price. Add installation, training, spare parts, software support, film waste, cleaning time, and planned maintenance. In production reviews, hidden downtime often costs more than a modest energy difference. Ask for a five-year cost model and verify each assumption. I once focused too heavily on hourly speed and underestimated changeover labor. That was a useful mistake. Inspect access to wear parts, review service response procedures, and speak with current operators when possible. Their practical experience may reveal noise, awkward adjustments, or frequent minor stops that specifications never mention.