AirAccess Access Control as a Service Platform with Auto-Cell Networking (ACasS)
Enterprise Hosted Platform - MVPAccess™
New! Napco Access 1 & 2-Door Controllers
Please contact us directly or visit our FAQ page or Video Library.
Toll Free 800-645-9330
Phone 631-842-9400
Fax 631-842-9135
Email: sale@safehomeexpert.com
sale@safehomeexpert.com (Latin America)
Sign up for integrator training seminars. 2 days and 3 day online courses are available from our directory indexed by product.
Learn MoreOffer the one access control solution powerful and flexible enough to protect all of your clients. Continental Access provides state-of-the-art access control software and hardware in an easy-to-implement and easy-to-use access control solution that seamlessly integrate with a wide range of facility management products.
Learn MoreA Plastic Coating Machine applies a controlled layer of polymer onto film, foil, paper, fabric, or shaped components. It may use extrusion coating, roll coating, spray coating, or hot-melt application. Each method creates a different surface finish, thickness, and bonding result.
Tim A. Osswald, a respected plastics-processing educator and author, describes the field clearly: “Plastics processing is both science and art.” That observation fits coating equipment well. The machine depends on measurable settings, yet practical judgment still matters. Operators adjust temperature, line speed, nip pressure, die gap, and cooling conditions. A small change can create streaks, pinholes, edge buildup, or weak adhesion.
The process usually begins with polymer preparation. A heated barrel melts the resin, while screws transport it toward a die or coating head. The coating head spreads the material across a moving substrate. Rollers then control contact and thickness. Cooling may follow immediately, leaving a stable protective layer.
The details are visible.
A smooth web enters the machine. A glossy film leaves it.
Modern systems add sensors, automatic thickness controls, and closed-loop temperature monitoring. These features improve repeatability, but they do not remove every risk. Material moisture, uneven tension, or poor surface preparation can still reduce performance. That is where real operating experience becomes valuable.
This guide explains what a Plastic Coating Machine does, how its main components work, and why process control affects product quality. It also examines limitations that manufacturers sometimes overlook. No machine is perfect. The best results come from matching equipment, polymer, substrate, and production goals carefully.
What Is a Plastic Coating Machine and How Does It Work?
A plastic coating machine applies a controlled polymer layer to film, fabric, paper, metal, or molded parts. Common systems use rollers, slots, spray heads, or extrusion dies. The selected method depends on viscosity, substrate shape, production speed, and required finish. For thin protective layers, the machine meters liquid coating through a narrow gap. A curing oven, UV unit, or cooling section then stabilizes the surface.
The practical coating range is often 10–200 μm. A 10 μm layer may improve moisture resistance without changing flexibility. A 200 μm layer offers stronger insulation, abrasion resistance, or chemical protection. Thickness control is not only a machine setting. Viscosity, web tension, line speed, temperature, and surface energy also affect the final result. ISO 2808:2019 describes several coating-thickness measurement methods, while ASTM D7091 supports nondestructive dry-film measurements on suitable substrates.
The numbers look precise. Production is less polite. A 50 μm target can vary across the web if the die lip is misaligned or the material heats unevenly. Operators therefore compare readings at the center and edges, rather than trusting one measurement. The World Bank’s What a Waste 2.0 report estimates that global municipal solid waste could reach 3.40 billion tonnes annually by 2050. This pressure makes thinner, functional coatings increasingly attractive, although reducing thickness too far can shorten product life. Calibration records, sample checks, and realistic tolerance bands remain essential.
Typical operating ranges and process characteristics for continuous plastic coating systems
| Process Dimension | Typical Range or Value | How It Affects Coating Performance | Common Measurement or Control Method |
|---|---|---|---|
| Coating thickness | 10–200 μm | Determines barrier protection, surface appearance, flexibility, weight, and material cost. | Wet-film gauge, dry-film gauge, gravimetric calculation, or inline thickness sensor. |
| Coating materials | Thermoplastics, solvent-based polymers, water-based polymers, hot melts, and reactive coatings. | The resin influences adhesion, chemical resistance, heat resistance, flexibility, and drying or curing requirements. | Material specification, viscosity check, solids-content test, and temperature monitoring. |
| Typical substrates | Plastic film, paper, foil, nonwoven material, textiles, molded parts, and metal strip. | Surface energy, roughness, cleanliness, and flexibility affect wetting and bond strength. | Surface inspection, dyne testing for films, cleaning verification, and adhesion testing. |
| Application methods | Roll coating, knife coating, slot-die coating, spray coating, dip coating, extrusion coating, and curtain coating. | The applicator determines coating uniformity, edge control, usable viscosity range, and achievable speed. | Gap setting, pump flow control, roll speed ratio, die pressure, or spray-flow adjustment. |
| Line speed | Approximately 5–150 m/min for many continuous coating lines. | Higher speed improves throughput but reduces available drying, leveling, and curing time. | Variable-frequency drive, servo control, encoder feedback, and synchronized web handling. |
| Coating width | Approximately 100–2,000 mm, depending on machine configuration and substrate format. | Width influences production capacity, material consumption, edge-trim requirements, and dryer sizing. | Adjustable guide rollers, applicator width, edge dams, masking, or trimming systems. |
| Material viscosity | Often about 10–10,000 mPa·s, depending on application technology and formulation. | Viscosity affects pumping, leveling, edge definition, coating weight, and surface defects. | Rotational viscometer, temperature-controlled reservoir, and metering-pump adjustment. |
| Drying or curing temperature | Approximately 40–180°C for many polymer coating processes. | Temperature controls solvent or water removal, melt flow, crosslinking, adhesion, and substrate protection. | Multi-zone oven controls, infrared heating, hot-air circulation, and thermocouples. |
| Drying or curing time | Typically a few seconds to several minutes. | Insufficient time can cause blocking, residual solvent, poor hardness, or weak adhesion. | Oven length, air velocity, line speed, infrared power, and residual-solvent testing. |
| Surface treatment | Corona, plasma, flame treatment, primer application, or mechanical preparation. | Raises surface energy or improves compatibility so the coating wets and bonds more reliably. | Dyne pens, contact-angle testing, treatment-power monitoring, and cross-hatch adhesion tests. |
| Typical quality checks | Thickness, coating weight, adhesion, gloss, haze, hardness, flexibility, and surface uniformity. | Confirms that the finished coating meets functional and visual requirements. | Micrometer, gravimetric test, cross-hatch test, gloss meter, haze meter, and visual inspection. |
| Primary machine sequence | Unwind → clean or treat → apply coating → level → dry or cure → cool → inspect → rewind. | Each stage contributes to stable thickness, adhesion, appearance, and finished-roll quality. | PLC or control system with sensors for speed, temperature, tension, pressure, and coating weight. |
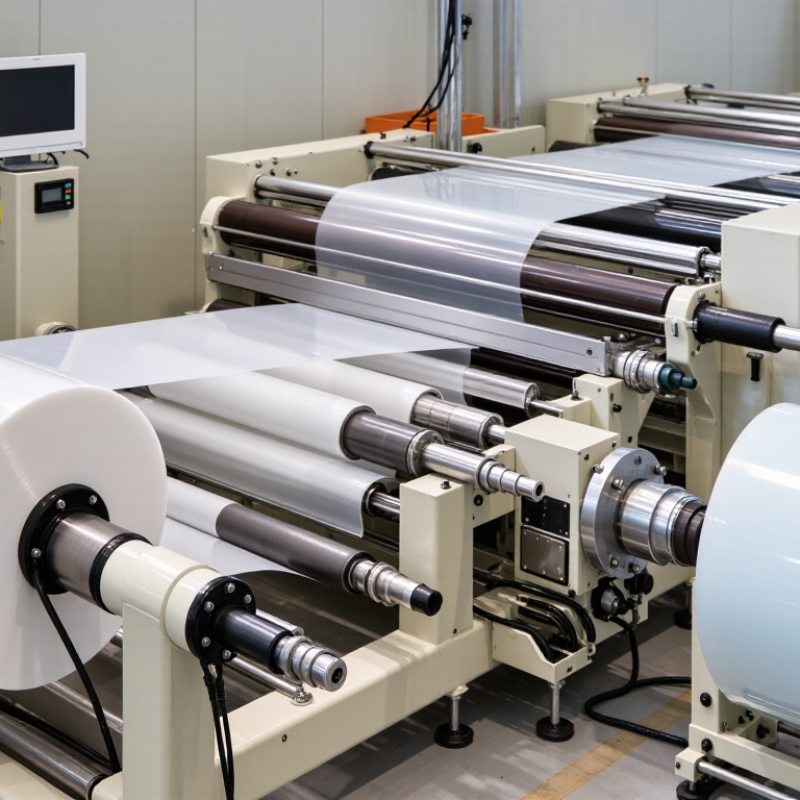
A plastic coating machine applies a controlled liquid layer onto a moving film web. The process usually begins with unwinding, web cleaning, and surface treatment. Corona treatment improves adhesion on low-energy films. A gravure, reverse-roll, or slot-die station then meters the coating. Drying ovens remove solvents or water through several temperature zones. Chill rolls stabilize the film before inspection and rewinding.
At 50–300 m/min, tension control becomes critical. A small tension change can create wrinkles, coating streaks, or uneven thickness. Operators monitor web speed, viscosity, oven temperature, airflow, and coating weight continuously. A practical target may be 1–5 g/m² of dry coating, depending on barrier, sealing, or print requirements. Speed is not everything. Excessive drying can deform the film, while insufficient drying leaves residual moisture.
The scale is significant. PlasticsEurope reported global plastics production of 413.8 million tonnes in 2023 in Plastics—The Fast Facts 2024. Smithers’ The Future of Flexible Packaging to 2028 also identifies continued demand for higher-performance flexible films. These reports support the need for efficient coating lines, but production data still requires caution. A laboratory recipe rarely transfers perfectly to full speed. Film structure, ambient humidity, and operator experience can change the result. Some defects remain difficult to predict. That is why trial runs, sample testing, and documented process checks remain essential.
A plastic coating machine applies a controlled polymer layer to film, foil, paper, or shaped parts. Its rollers guide the substrate while controlling pressure, speed, and coating thickness. In practice, a clean roller surface matters as much as the polymer formula. Dust can create thin streaks, pinholes, or uneven gloss.
The die places polymer across the material’s width through a narrow opening. Its gap and internal flow must remain consistent. Operators often adjust temperature and pressure because viscosity changes during production. A small setting error can leave heavier edges or weak coverage near the center. That detail is easy to underestimate.
Air knives refine the wet layer after application. A narrow, high-speed air stream removes excess polymer and smooths the surface. The air gap, angle, and pressure affect coating weight. Too much air may cause waves or exposed spots. Too little air leaves ridges behind. I have found that stable tension and gradual speed changes improve results, although no setup is perfectly forgiving. Quality checks should measure thickness across several points, not just one convenient location. Calibration records, sample testing, and careful visual inspection help connect machine settings with reliable coating performance.
A plastic coating machine applies a controlled layer of polymer material to metal, fabric, paper, or plastic parts. Rollers, spray heads, or dipping systems distribute the coating evenly. The coated surface then enters a heated drying or curing chamber. Airflow, conveyor speed, and film thickness all affect the final result.
Drying removes liquid carriers, while curing strengthens the coating through chemical or thermal changes. Working temperatures commonly range from 80°C to 200°C. Lower temperatures may suit moisture removal or heat-sensitive substrates. Higher temperatures can support faster curing and stronger surface bonding. However, the chamber setting does not equal the product temperature. A thick part may remain cool inside while its outer layer appears finished.
Temperature control needs evidence. Technicians often check several points with calibrated sensors, not only the oven display. They also inspect gloss, adhesion, hardness, and surface bubbles after cooling. Poor airflow can leave wet patches. Excessive heat can cause discoloration, warping, or trapped solvents.
Small details matter.
Coating suppliers usually provide a recommended time-temperature window, but real equipment may behave differently. Conveyor speed, exhaust volume, ambient humidity, and substrate shape can shift the outcome. A useful production record should connect these variables with test results. Simplified settings are convenient, yet they can mislead. Careful trials remain necessary when changing materials or film thickness.
A plastic coating machine spreads a liquid polymer across film, foil, or fabric. Sensors make this process measurable. Without them, operators may rely on visual checks and late adjustments. A thickness sensor scans the coated web as it moves. It detects thin spots, heavy bands, and uneven edges. The control system then adjusts the coating gap, pump rate, or line speed. Small changes matter when the coating is only a few microns thick.
Tension sensors monitor the web between rollers. Load cells detect pulling force and send data to the drive system. If tension rises, the film may stretch or wrinkle. If it falls, the web can wander or sag. Feedback controls correct roller speed in real time. In practical production, clean sensor surfaces and stable mounting are essential. Dust can create false readings. Vibration can also confuse the measurement.
Coating accuracy depends on several signals working together. Thickness data shows the result, while tension data explains part of the cause. Temperature sensors add another layer, because viscosity changes with heat. Readings can drift. A calibration check before each run is sensible, although busy teams sometimes skip it. That shortcut has caused avoidable waste in my experience. Sensors improve consistency, but they do not replace trained judgment. An operator still needs to inspect the wet coating, edges, and finished roll. Errors often appear where the system assumes conditions are stable.